How to Design Translucent Parts for LED Collectibles
A practical guide to material, diffusion, paint, light control, assembly and testing decisions for translucent parts in LED collectibles.
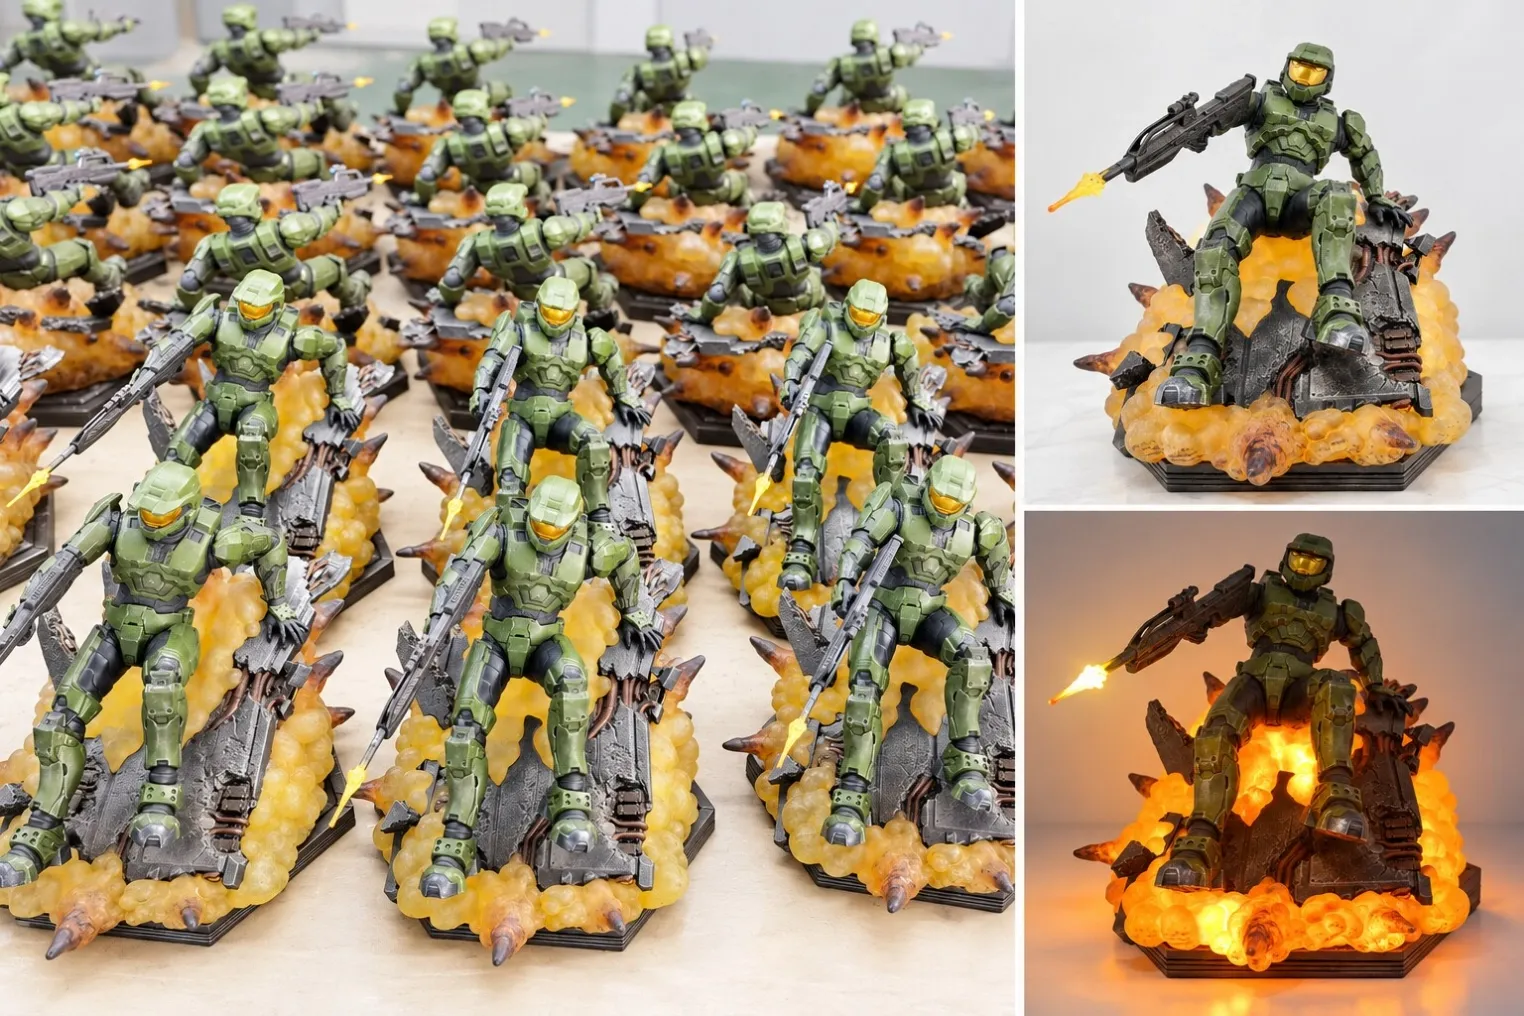
The practical answer: translucent parts for an LED collectible should be engineered as part of the lighting system, not added after the sculpt and electronics are finished. Material, wall thickness, surface texture, color, paint coverage, LED position, internal structure and assembly all change the final effect. The safest route is to define the intended appearance early, prototype it with representative materials and finishes, and approve the illuminated result before tooling and production.
A clear or translucent component can look convincing when unlit but expose hotspots, dark areas, internal hardware or light leaks when powered. The opposite can also happen: a part may glow evenly but lose sculpted detail or look too cloudy in normal display. The design has to work in both states.
Start With the Visual Effect, Not the LED
Before selecting components, define what the customer should see. Is the part meant to emit a soft internal glow, show a bright energy core, illuminate an engraved pattern, or transmit light only through selected openings? Each effect requires a different relationship between the light source and the visible surface.
Questions to answer before engineering begins
- Which surfaces should glow, and which must remain opaque?
- Should the LED itself be visible or completely diffused?
- Does the effect need to look uniform from all viewing angles?
- What color should the part have when the power is off?
- How bright should the effect appear in normal indoor lighting?
- Will paint, decals, metallic layers or weathering cover any translucent areas?
- Where can wires, switches, batteries and access panels be hidden?
A clear visual target gives the engineering team something measurable to build toward. Without it, brightness becomes the only discussion even though the real problem may be diffusion, light leakage or the off-state appearance.
Choose the Translucent Material Around the Product
Transparent and translucent resin, PVC or ABS components do not behave identically. The appropriate choice depends on the size and shape of the part, required detail, structural load, production process, finish and the way the light must travel through it.
Resin can suit detailed translucent effect pieces and lower-volume complex forms, but thick sections, trapped air, color consistency and handling of fragile projections require attention. PVC/ABS may be appropriate for molded production parts, but wall thickness, draft, gates, weld lines and the final assembly route have to be considered before tooling.
Material selection also affects the surrounding product. A rigid transparent insert may need a concealed key or mechanical support. A flexible part may distort at a paint boundary. A large clear component can reveal glue, joints and internal structures that would be invisible inside an opaque part.
Wall Thickness Controls Both Light and Appearance
Thickness is not only a structural value. It changes color density, transmission and diffusion. A thick area may appear darker than a thin edge. Sharp changes in section can create uneven glow, and deep sculpted features can produce unexpected shadows.
The 3D file should therefore be reviewed in illuminated form as well as a conventional solid model. Long light paths, narrow channels, undercuts and solid masses should be identified before prototype work. If the design requires even illumination, the internal geometry may need hollowing, controlled thickness, a diffuser or multiple light sources.
Common geometry risks
- A single LED creates a bright hotspot directly behind the surface.
- Thick decorative details appear muddy or noticeably darker.
- Internal ribs, screws or wires become visible when illuminated.
- Light cannot reach a remote tip or branch of the effect piece.
- A joint interrupts the light path or forms a dark ring.
- Thin edges become much brighter than the intended focal area.
Diffusion Must Preserve the Sculpt
Diffusion helps spread light and reduce hotspots, but too much can flatten detail and make the component look milky. It can be created through the material itself, an internal diffuser, surface texture, a coating or controlled distance between the LED and the visible part.
The correct solution depends on where the sculpted detail lives. If the outside surface carries fine texture, aggressive frosting or heavy coating may soften it. An internal treatment may preserve the exterior but be difficult to apply consistently. A separate diffuser can improve serviceability but adds components, tolerances and assembly operations.
These decisions should be tested on a representative physical part. A plain flat sample does not show how the actual curves, recesses, wall thickness and paint boundaries affect the light.
Paint and Finish Define Where the Light Can Travel
Translucent collectibles often combine transparent, tinted, opaque and metallic areas in one component. Paint is therefore part of the optical structure. A thin tinted layer can shift the color of the material; an opaque layer can block light; a metallic coating can reflect it internally or reveal pinholes and uneven coverage.
Paint masks and boundaries need to be planned around the sculpt and assembly. If the light-stop layer ends at an exposed seam, small alignment differences can create a bright line. If an opaque coating covers a mating surface, paint thickness may change the fit or scrape during assembly.
Finish controls worth approving on the physical sample
- Color and clarity in both powered and unpowered states
- Uniformity of translucent tint across the full part
- Opacity of areas intended to block light
- Clean transitions between glowing and non-glowing surfaces
- Visibility of fingerprints, sanding marks, dust or adhesive
- Resistance to handling during assembly and final QC
The approved sample should be viewed under consistent ambient lighting and from the angles customers are likely to see. Photographs alone can hide hotspots or exaggerate brightness.
Control Light Leaks Before Final Assembly
Light leaks commonly appear at parting lines, screw points, switches, battery covers and joints between translucent and opaque parts. They are often treated as cosmetic defects, but the cause may be structural: insufficient overlap, uncontrolled gaps, thin paint coverage or a light source positioned too close to a seam.
Opaque internal barriers, stepped joints, controlled overlap and planned light-stop coatings can help. The design should avoid relying on adhesive alone to block light. Glue quantity varies, may remain visible through a clear part and can complicate rework.
Fit checks should be performed with production-representative finishes applied. Bare prototypes may close correctly while painted parts leave a gap or scrape during assembly.
Plan Electronics, Access and Assembly Together
LED modules, wiring, switches and power components need secure locations that do not interfere with the sculpt or make the visible part difficult to assemble. The route should protect wires from pinching, keep soldered connections away from mechanical stress and allow the product to be tested before it is permanently closed.
Assembly sequence matters. If the light module becomes inaccessible before the translucent part is fitted, faults discovered later require destructive rework. A better sequence provides defined checkpoints: electronics test, subassembly test, illuminated fit check, cosmetic inspection and final functional QC.
For mixed-material collectibles, metal supports, resin housings, PVC/ABS shells and decorative parts may all meet around the lighting system. Their tolerances and fastening methods need to be resolved as one product rather than separate component drawings.
Prototype the Real Stack-Up Before Tooling
A useful lighting prototype should represent more than the LED. It should include the actual or closely representative translucent material, wall thickness, surface treatment, paint layers, internal spacing, structural barriers and assembly joints.
During development, review the following conditions:
- Powered and unpowered appearance
- Normal room light and darker viewing conditions
- Front, side and rear viewing angles
- Hotspots, dark zones and visible internal components
- Color shift caused by material and coatings
- Light leakage around joints and controls
- Assembly stability and repeatable alignment
- Functional operation after repeated handling
Our collectible development and production process connects prototyping, engineering, finishing, assembly and QC so visual effects can be checked before the production route is fixed. Related mixed-material and functional work is shown on the Projects page.
Production Control Should Follow the Approved Effect
Once the illuminated sample is approved, production needs references for both appearance and function. Translucent material color, paint coverage, LED placement, wire routing and joint fit can all shift the result. Checking only whether the light turns on is not enough.
In-line inspection can compare translucent parts before assembly, verify opaque light-stop areas, test electronic subassemblies and inspect illuminated fit before final closure. Final QC should confirm operation, overall brightness pattern, visible finish, assembly alignment and cleanliness. Packaging should also prevent pressure or abrasion on clear and plated surfaces.
What Buyers Should Include in the Project Brief
A useful brief should identify the desired powered and unpowered appearance, approximate viewing conditions, light color, operating method, accessible controls, power arrangement and any critical material or finish requirements. Reference images are helpful, but they should be accompanied by a description of what must be reproduced.
If the visual effect is central to the product, allow approval stages for the optical prototype and finished illuminated sample. This reduces the risk of discovering after tooling that the material is too clear, the paint blocks too much light or the internal structure remains visible.
Frequently Asked Questions
Can a standard clear 3D print confirm the final LED effect?
It can help test geometry and component position, but it may not reproduce the transmission, diffusion, tint or surface finish of the production material. A representative material-and-finish prototype is still needed.
Should the brightest LED always be selected?
No. Higher brightness can make hotspots, leaks and internal components more visible. The goal is the approved visual effect, which depends on distribution, diffusion, color and viewing conditions as well as output.
When should translucent paint and light-blocking areas be approved?
They should be reviewed on an assembled, illuminated sample before final production approval. Boundaries and coating thickness can affect both appearance and fit.
For a review of a translucent or functional collectible, send us your project scope with the intended material, scale, lighting effect, finish and operating requirements.